- Phone
-
Address
128 Tongxing North Road, Beibei District, Chongqing
Product Categories
Chongqing Danduo Technology Co., Ltd
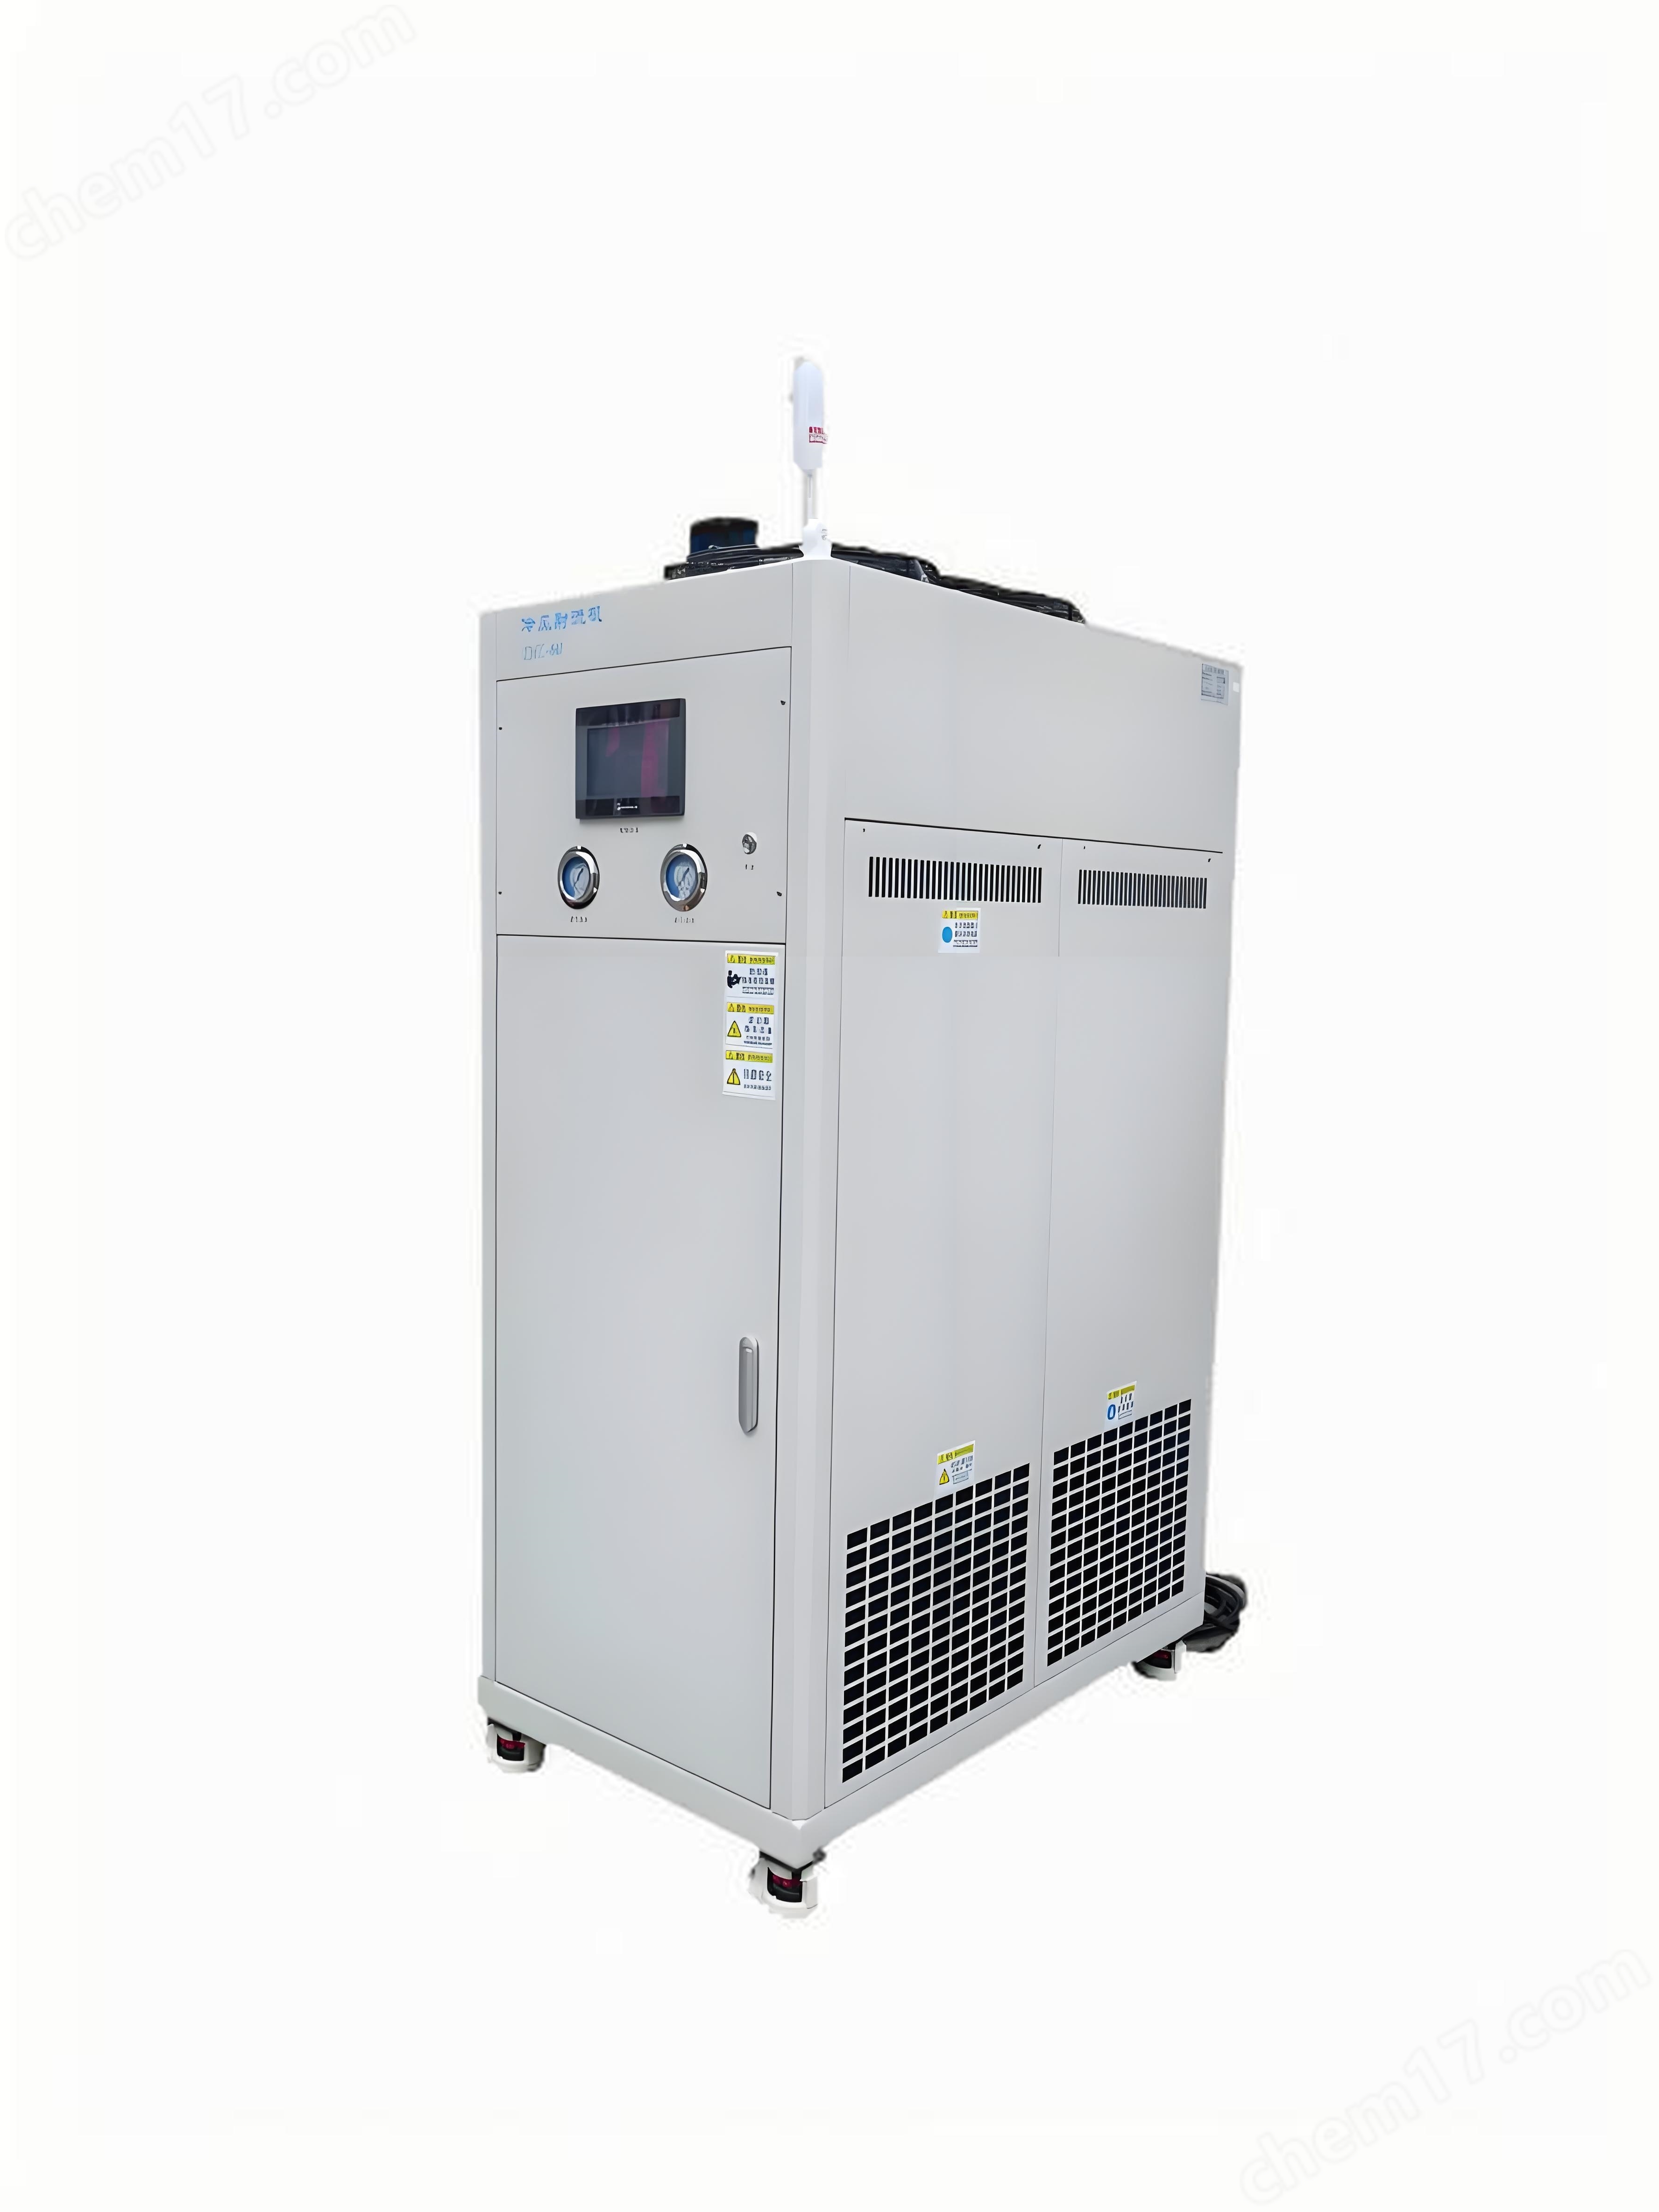

Micro lubrication cold air cutting processing - Chongqing Danduo Technology Co., Ltd
NegotiableUpdate on 05/06
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
Micro lubrication cold air cutting is an integration of low-temperature cold air cutting and micro lubrication cutting. By mixing cold air at -10 ℃ to -100 ℃ with micro lubricating oil to form a mist, it is directly sprayed into the cutting area to achieve efficient cooling and lubrication.
Product Details
Micro lubrication cold air cutting processingLow temperature micro lubrication cutting technology is an integration of low-temperature cold air cutting and micro lubrication cutting. By mixing cold air at -10 ℃ to -100 ℃ with micro lubricating oil to form an aerosol, it is directly sprayed into the cutting area to achieve efficient cooling and lubrication. The processing can be divided into the following key steps:
Composition and preparation of micro lubrication cold air cutting machining system
Gas source and refrigeration system
Air source: Compressed air or nitrogen is purified through coarse filtration and enters the refrigeration system to cool down to the target temperature (such as -40 ℃ to -50 ℃).
Refrigeration methods: including indirect refrigeration through cyclic compression, indirect refrigeration through low boiling point media, direct refrigeration through adiabatic expansion of air, or semiconductor refrigeration to ensure stable and controllable cold air temperature.
Insulated pipeline: Transport low-temperature gas to the processing area to reduce temperature loss in intermediate links.
Micro lubrication supply system
Lubricant selection: Environmentally friendly trace lubricants (such as vegetable oil, synthetic esters, or polyethylene glycol) are used, with a typical dosage of 10-20 milliliters per hour, significantly lower than traditional cutting fluids.
Atomization device: Mix lubricating oil with cold air through a single or dual channel system to form a micrometer sized mist (particle size generally controlled below 2 μ m), ensuring uniform spraying to the cutting point.
Cutting machining system
Machine tool adaptation: Choose an internal or external liquid supply system based on the type of machine tool (such as CNC lathe, machining center). Built in integrated into the spindle bore for better cooling effect, but machine tool modification is required; External positioning through independent nozzles, high flexibility.
Tool selection: Prioritize using internal cooling tools (such as internal cooling drill bits and milling cutters) to ensure that the gas mist directly reaches the cutting interface.
The process of micro lubrication cold air cutting machining
1. Preparation stage
Choose appropriate equipment: Ensure that the machine tool is equipped with a micro lubrication system and a cold air supply device.
Preparation of materials: Prepare the workpiece to be processed and suitable cutting tools according to the processing requirements.
Check equipment status: Confirm that all equipment (including MQL system, cold air generator, etc.) are in good working condition and connected correctly without leaks.
2. Configure parameters
Set MQL parameters: Adjust the fuel injection quantity, frequency, and other parameters of the MQL system based on the characteristics of the processed material and process requirements.
Set cold air conditions: Adjust the pressure, temperature, and flow rate of the cold air supply device to adapt to different cutting speeds and feed rates.
3. Start processing
Start the machine tool: First, turn on the machine tool and let it reach a stable working state.
Enable MQL system: Before starting cutting, activate the micro lubrication system to ensure that an appropriate amount of lubricating oil can be accurately sprayed onto the tool workpiece contact point.
Supply cold air: Immediately start the cold air supply device to provide low-temperature air flow to the cutting area for cooling.
4. Real time monitoring
Monitoring the cutting process: closely monitor the changes in chip morphology, surface smoothness, and cutting force generated during the cutting process.
Adjust parameters: If necessary, adjust the parameter settings of MQL and cold air in a timely manner to optimize the processing effect.
5. End processing
Stop oil and gas supply: After completing the scheduled cutting task, first turn off the MQL system and cold air supply device.
Clean up the site: Remove the processed workpieces and perform necessary cleaning and maintenance on the machine tool.
Maintenance matters
Regularly check the MQL system: ensure that the nozzle is unobstructed and avoid affecting the lubrication effect due to blockage.
Keep the cold air device clean: Regularly clean the filters inside the cold air supply device to prevent dust from entering the system and affecting performance.
Lubricate moving parts: For systems or cooling devices containing moving parts, perform regular lubrication and maintenance according to the manufacturer's recommendations.
Record maintenance activities: Establish detailed maintenance logs to record the specific content, date, and executor information of each maintenance, facilitating the tracking of equipment status.
Similar Product Recommend

