-
E-mail
1040308642@qq.com
-
Phone
13971637109
-
Address
No. 3 Xinhua Avenue, Wuhu Industrial Park, Wuhan City
Product Categories
Wuhan Electric Furnace Co., Ltd

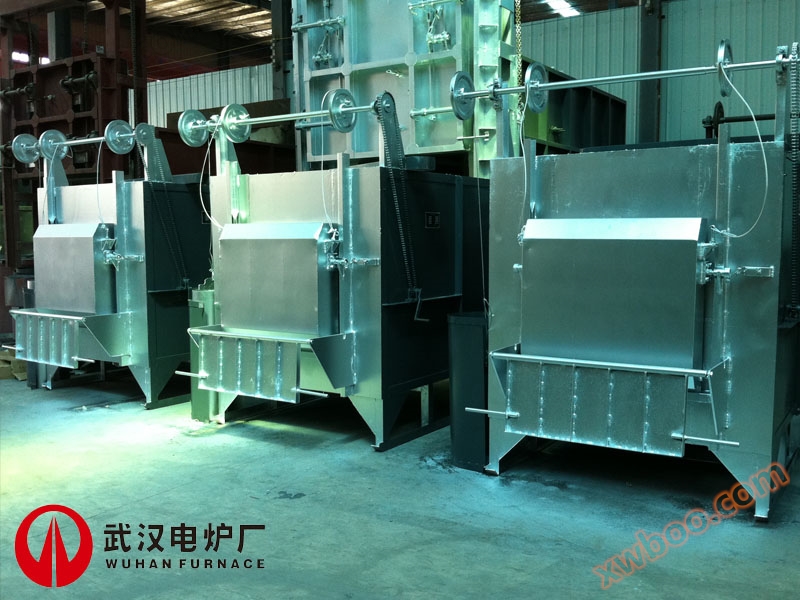
Pressure vessel gas heat treatment furnace
NegotiableUpdate on 11/23
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
※ Product Usage: This series of pressure vessel gas heat treatment furnaces uses natural gas heating and is mainly suitable for heat treatment of large shafts, forgings, cast steel parts, pressure vessels, and large welded parts in the metallurgical, mechanical, and chemical equipment heat treatment industries
Product Details
|
※Product Usage
This series of pressure vessel gas heat treatment furnaces uses natural gas heating and is mainly suitable for heat treatment of large shafts, forgings, cast steel parts, pressure vessels, and large welded parts in industries such as metallurgy, machinery, and chemical equipment.
※Product Features:
1.The combustion medium is heated by natural gas, which is fully burned, pollution-free, and has a fast heating speed. The maximum operating temperature can reach650-1200℃, smoke emissions comply with《GB9078-88Emission Standards for Smoke Layer of Industrial Kilns;
2.The furnace lining adopts an alumina ceramic fiber module structure, which has low heat storage, low heat loss, and significant energy saving;
3.Heating adopts high-speed pulse burners, evenly distributed on both sides. Continuous proportional adjustment combustion, the actuator adjusts the size of the air flow, and the gas volume is adjusted through a proportional valve. To achieve air-fuel ratio combustion, there are lower limit limits for gas and air volume, and control solenoid valves are installed on the gas pipes of each burner. Each burner is equipped with an independent and complete combustion controller, which has automatic ignition, flame detection, fire alarm, and automatic gas cut-off. This fully ensures the stability and safety of the combustion temperature control system.
4.Waste heat utilization: Preheating the hot air temperature in the air duct by passing the high-temperature flue gas in the furnace through a heat exchanger250-300℃, then sent into the furnace, greatly saving gas consumption and production costs;
5.The furnace door of the gas heating furnace adopts a combination frame structure of high aluminum full fiber refractory silk blanket and heat-resistant steel, with an electric hoist for lifting and lowering. The sealing mechanism of the furnace door adopts a long and short lever spring type automatic compression cam mechanism(Optional electric cylinder compression device)And the soft edge sealing device. Ensure frictionless up and down, effortless, safe and reliable.
6.The refractory masonry of the trolley adopts a high alumina shaped brick structure, which has good sealing effect with the furnace body and high compressive strength. The trolley surface is equipped with shims for stacking workpieces, and the trolley frame is made of heat-resistant steel to ensure that the vehicle body does not deform and is durable. The electric push rod (or cylinder) of the sealing block between the furnace body and lining has an automatic compression structure, and the opening and closing of the side and seal are interlocked with the entry and exit of the furnace car.
7.Control system: adopting intelligent technologyPLCComputer-controlled automatic control
7.1.Furnace temperature control system:
Adopting advanced intelligent digital temperature controller. It forms a closed-loop control system with temperature measuring components and automatic control burners. Temperature controller interface and upper levelPCpassR485(RS422)Bus connection, forming an intelligent temperature control system for heat treatment furnaces. superiorPCThe machine adopts industrial control computer and high-resolutionLCDMonitor, equipped with self-developedHMIMonitoring software ensures that the entire system has a user-friendly interface. Adopting advanced fuzzy control principles, it has high precision, high flexibility, anti-interference ability, and high reliability. The temperature control system can automatically calculate, operate, display, and store the heat treatment production process curve, achieving full process control.
7.2.Furnace pressure automatic control system:
The furnace pressure can be set and automatically adjusted to control it at the optimal value, ensuring stable furnace conditions and fully utilizing furnace gas heat.
7.3.Pipeline parameter self-control system
The pressure of the combustion air and fuel pipelines required for the combustion system can be set and automatically adjusted to control the optimal ratio of combustion air and fuel, ensuring extremely high combustion efficiency and eliminating black smoke.
7.4.Reliable security protection system:
The instrument cabinet is equipped with temperature, furnace pressure, operating value displays for each burner and pipeline parameter, as well as abnormal situation alarms and emergency protection measures to ensure operational safety.
8.Centralized control system
Adopting high-precision Siemens technologyPLCAs the core unit of the entire furnace temperature control system. The control of temperature, pressure, and combustion air pressure inside the furnace is entirely managed byPLCCompleted. This reduces various instruments such as temperature control, digital adjustment, manual controllers, digital displays, etc., greatly reducing the complexity of the entire system configuration.
superiorPCThe machine adopts industrial control computer and high-resolutionLCDMonitor, equipped with self-developedHMIMonitoring software enables the entire system to have a good user interface while monitoring several furnaces or furnaces that require upper computer monitoring (two or more)PCThe advantage of monitoring one or several furnaces simultaneously is that onePCWhen the machine malfunctions without affecting the normal operation of the entire system, the software can easily meet the requirements.
|
|||||||||||||||
 |
 |
||||||||||||||
|
※Technical Specifications:
Product Model
Gas consumption
Temperature ℃
burner
Number of districts
Furnace sizemm
loading capacityt
Gas powered car annealing furnace
≤250Nm3/h
750
14branch
7
14700×3600×3600
100
|
|||||||||||||||
※Typical user: Yuchai Group Suizhou Dongte
Wuhan Honglang